Monthly Archives

October 2026

The Shear Dilemma

By UncategorizedNo Comments

Every scrap yard eventually confronts the same question: which shearing machine actually pays for itself? As induction furnaces and steel mills push for denser, more consistent charge material, the choice of processing equipment has shifted from a routine purchase into a decision that shapes plant economics. What follows sets three widely used shearing technologies side by side — the multi-blade shear, the box shear, and the container shear — and uses real specification data to show why compression-based shearing is the sounder investment for most operations.

The Scrap Processing Challenge

Raw scrap arrives in every shape and density imaginable: pipes, structural sections, machinery frames, sheet offcuts, and mixed light-to-heavy loads. Left as it is, this material is costly to transport, slow to charge, and uneven to melt. The job of a shearing machine is to cut and compress it into dense, uniformly sized pieces that move cleanly from yard to furnace.
How a shear achieves that varies considerably from one design to the next, and the technology a yard selects bears directly on output density, throughput, operating cost, and — the figure that matters most — cost per ton processed. The three machines examined here look broadly similar on paper, yet they behave very differently on the floor.

Multi-Blade Shear — Density and throughput, at the lowest cost per ton

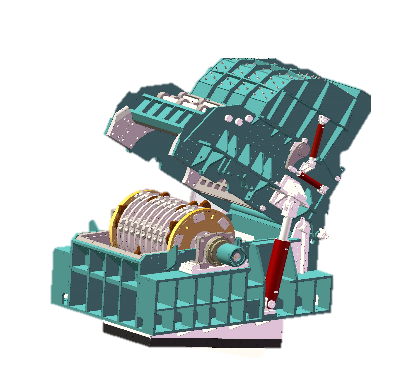
The multi-blade shear pairs lid compression with a top-clamp ram, forcing scrap into a reinforced chamber where several blades cut it in a single stroke. Because the charge is compacted before it is cut, the machine copes comfortably with a broad mix of feed, from medium sections through to heavy structural scrap, reducing it to pieces under 500 × 500 mm and handling up to five pieces in one chamber load. Output density sits at roughly 1,000 kg/m³, and operating cost runs as low as ₹90 per ton — the lowest of any shear in this comparison.

Key Components

▪ Compression Chamber — heavy-duty steel chamber with lid and top-clamp rams
▪ Multi-Blade Cutting Head — several blades shearing at once for shorter cycle times
▪ Feed Cylinder — draws scrap into the chamber for continuous processing
▪ Hydraulic Power Pack — pumps, valves, and reservoir driving every compression and shear function
▪ PLC Control Panel — automatic and manual cycle control with integrated safety interlocks

Box Shear — Most dense output in the range

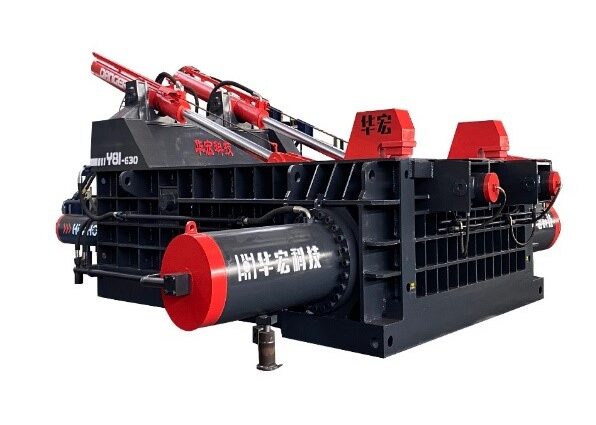
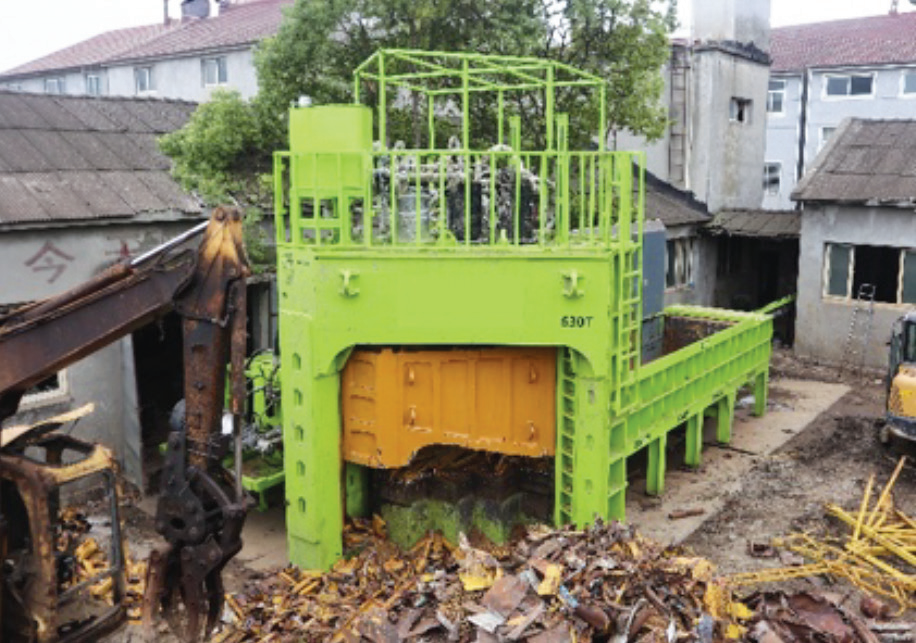
The box shear adds a third axis of compression. Lid, side, and top-clamp rams consolidate scrap from every direction before the blades make their cut, producing some of the densest output of any shear category — around 1,200 kg/m³. That three-way action lets it take on the same medium-to-heavy, mixed feed as the multi-blade shear while cutting oversized material down from 1,200 mm to 500 mm in a single chamber load. Where maximum density is the priority, no machine in the range performs better.
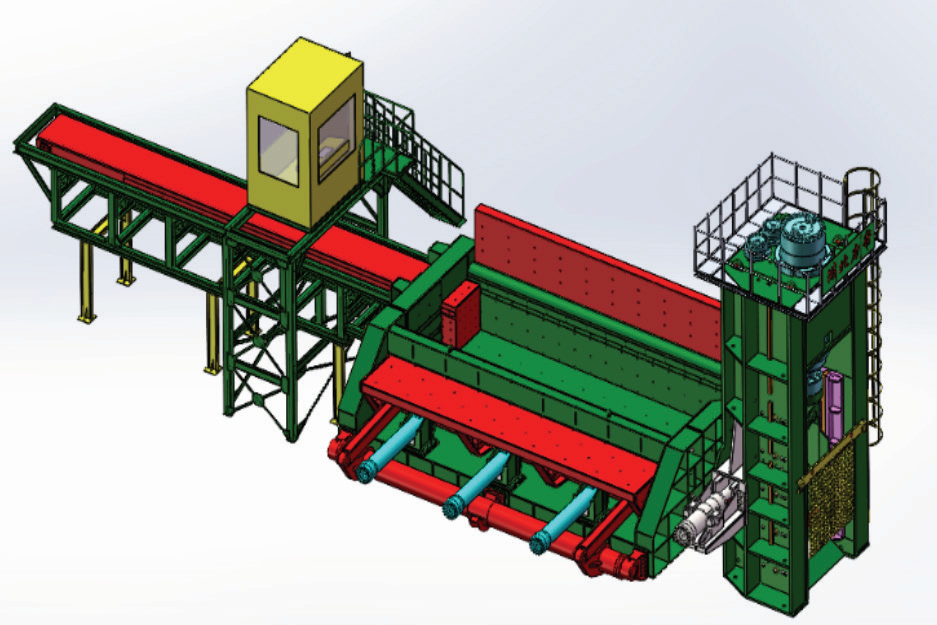
Key Components

▪ Compression Chamber — heavy-duty steel chamber with lid, side, and top-clamp rams
▪ Multi-Blade Cutting Head — multiple blades shearing the compacted charge in one stroke
▪ Feed Cylinder — draws scrap into the chamber for continuous processing
▪ Hydraulic Power Pack — pumps, valves, and reservoir driving every compression and shear function
▪ PLC Control Panel — automatic and manual cycle control with integrated safety interlocks

Container Shear — Simple and compact, at lower density

The container shear works on a simpler principle. Scrap is loaded into a closed, container-style chamber, compressed from the sides, and cut with a single horizontal stroke. It is mechanically straightforward and easy to run, but that simplicity carries trade-offs.
With side compression alone — and none of the lid or top- clamp action of the compression shears — the container shear settles at a noticeably lower output density of around 700 kg/m³. Lower density means more truckloads and more charging cycles to move the same tonnage, and processing capacity trails the other two machines at every comparable model tier.

Key Components

▪ Side Compression Rams — two horizontal cylinders compressing scrap inward
▪ Shear Blade Assembly — single shear head cutting the compressed charge
▪ Hydraulic Power Pack — pumps, motors, valves, and oil reservoir
▪ Safety Interlocks — emergency stops, proximity sensors, and limit switches

Head-to-Head: Density, Throughput, and Cost per Ton

Set against equivalent shear-force model tiers, the two compression shears consistently out-process the container shear while producing denser, more furnace-ready material. The table below shows how the three compare on the factors that shape
day-to-day economics.

Factor Multi-Blade Shear Box Shear Container Shear
Method Lid+top clamp Lid+side+top clamp Side only
Output density ~1,000 kg/m³ ~1,200 kg/m³ ~700 kg/m³
Operating cost ₹90 / t ₹120 / t ₹100 / t
Capacity range 10–35 tons/hr 10–35 tons/hr 8–20 tons/hr
Scrap suitability Medium, heavy, mixed Medium, heavy, mixed Medium & light only
Pieces per cycle Up to 5 per load Single piece per load Single-piece

The pattern holds across the range. At every matching model size, the compression shears move more tonnage per hour and pack it denser than the container shear. The multi-blade shear does so at the lowest operating cost of the three; the box shear trades a slightly higher running cost for the densest output in its class.

For yards handling mixed or heavier streams, both translate into better furnace charging efficiency and lower freight per ton — savings that usually outweigh any difference in operating cost.

The Verdict

The container shear remains a reasonable entry point for yards handling only light-to-medium scrap on a limited budget; it is simple, affordable, and easy to run. But for operations that need higher throughput and denser, more consistent output across a wider range of material, the multi-blade and box shear are the sounder long-term investment. In the end, the right choice follows the scrap — the heavier and more varied the stream, the stronger the case for compression-based shearing.

About Dev Energy

Dev Energy is a trusted provider of end-to-end scrap processing solutions for secondary steel melting plants, spanning shearing, scrap feeding, and fume extraction systems. Backed by more than two decades of engineering, over 200 completed projects, and a 100,000+ sq. ft. manufacturing facility, Dev Energy helps steel producers lower processing costs while improving scrap quality and furnace performance.
Coal Gasification: Driving Competitiveness Through Substitution of High-Cost Fuels like PNG, LNG, LPG, Propane, and Furnace Oil

By UncategorizedNo Comments

THE BIG PICTURE — WHY COAL GASIFICATION?

The Indian Industrial landscape is undergoing its most consequential energy transition in a century. There is huge shift of usage of conventional fossil fuels like Natural Gas, LPG, Propane or Furnace Oil to the usage of abundantly available coal in India. This conversion is happening through proven commercial scale available technological options on End application by using Coal Gasification route to create Coal Gas suitable as fuel. This offers the user long-term energy security along with economic benefits of de-risking the user from the fuel availability & price volatility shocks. This has created a once-in-a-generation window in India to fundamentally transform how India and the world produce steel, aluminium, ceramics, glass, chemicals and derivatives of same.

At the centre of this transformation sits a technology that is mature, commercially deployed, domestically adaptable, and strategically decisive: Coal Gasification. By converting India’s abundant coal reserves into a clean, high-quality Coal Gas coal gasification technology enables economic competitiveness of India’s most important industrial sectors without dependence on expensive, import-constrained Piped or Liquified Natural Gas, Liquified Petroleum Gas (LPG) and Furnace Oil.

PROGRESSIVE DEVELOPMENT - TECHNOLOGY

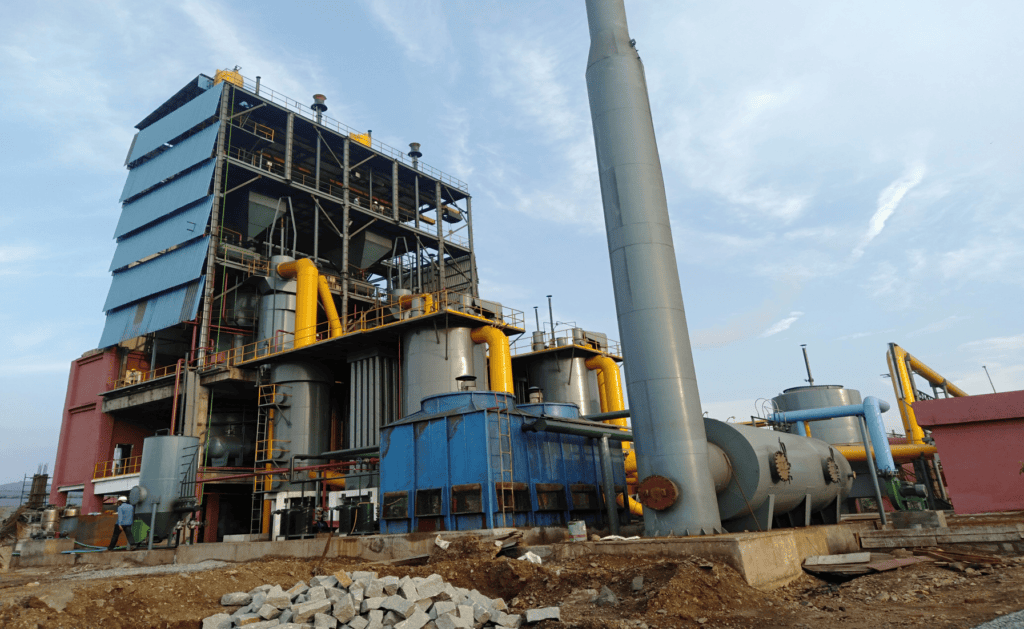
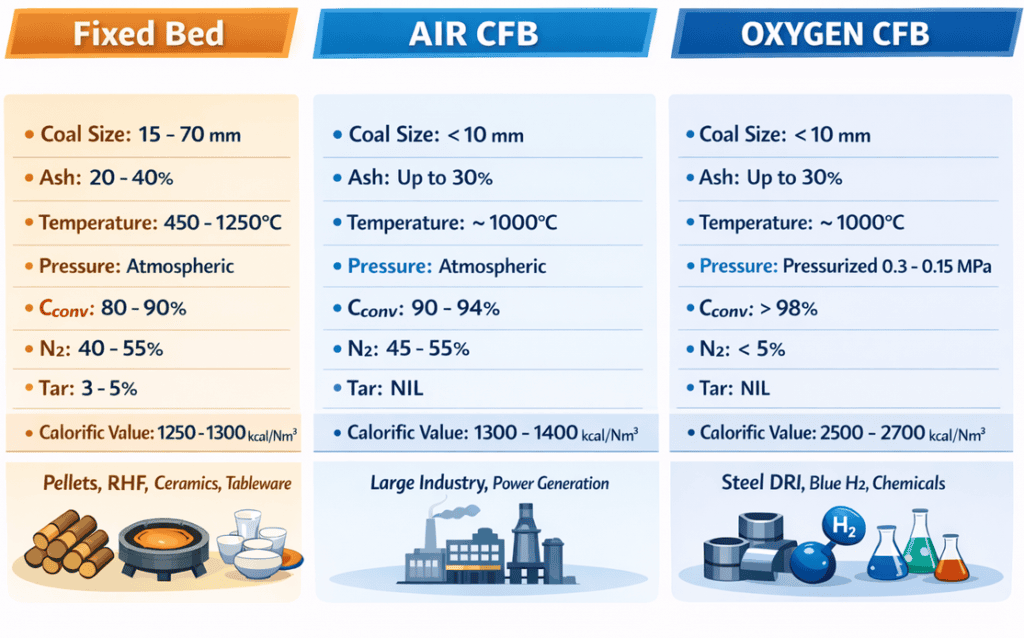
Coal emerging as the main INDUSTRIAL FUEL source in India has witnessed a journey from pilot to commercial scale applications in last two decades. The initial usage of Fixed Bed technologies has yielded huge benefits to Industry. Now, the latest Circulating Fluidised Bed Gasification technologies which having globally established itself is ripe for yielding benefits in India.

CORE COAL GASIFICATION TECHNOLOGIES

Coal Gasification at atmospheric pressure and with air as reagent is proven as the most technically suitable for generation of gas usable as fuel across all industries in India and Globally. Dev Energy, since 2003, has been pioneer inintroduction by of this technology in India in various industrial applications having cumulatively converted Indian coal over ~ 50 million tons into usable Coal gas as fuel.

MULTIPLE INDUSTRIES - APPLICATIONS

The Coal Gas generated from Indian coal which is then cleaned and cooled to be used as FUEL gas is used as a direct substitute to expensive, import-constrained Piped or Liquified Natural Gas, Liquified Petroleum Gas (LPG) and Furnace Oil in multiple industry segments.

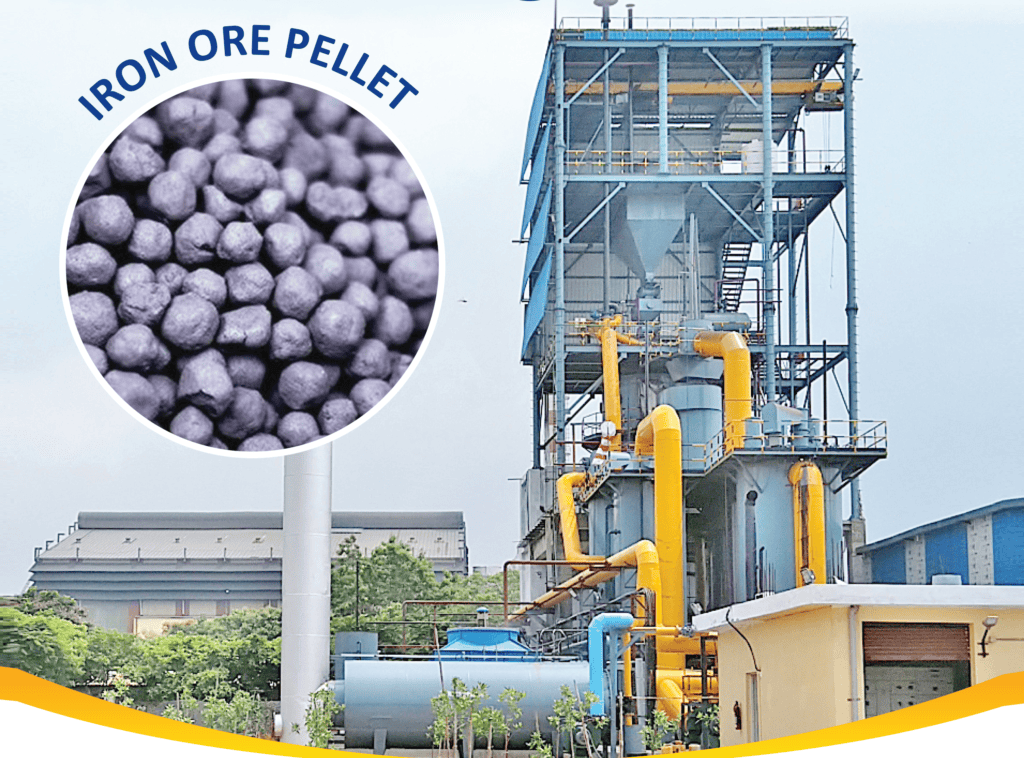
Steel Industry – Iron ore pelletisation Kilns with all three designs – Straight grate, Rotary Kiln and Circular Kiln need fuel to fire pellets at 1250 °C successfully replaced by Coal Gas

Steel Industry – Tunnel Furnaces for Slab Rolling mills need fuel for heating thin slabs to 1200°C successfully replaced propane by Coal Gas

Steel Industry – Reheating Furnaces for Rolling mills to producing long or flat steel need fuel for heating steel successfully using Coal Gas

Steel Industry – Stainless steel hot and cold rolling mill furnaces need a steady, controllable flame at 1050 °C successfully replaced LNG by Coal Gas

Refractory Industry – Tunnel kilns needed fuel to bake the refractory bricks successfully used Coal Gas

Ceramics Industry – Tiles and Tableware sector including Wall and floor tiles, bone China, sanitaryware and insulators kilns demand clean fuel and uniform firing successfully replaced LNG by Coal Gas

Glass Industry – horse shoe regenerative kilns need temperatures up to 1700 °C successfully operated with Coal Gas.

Alumina Industry – Calciners rotary kilns or flash calciners operating at 1100°C operating on Coal Gas.

Dev Energy has in last 24 years completed projects successfully in above industries providing end user with exceptional economic advantage.

FIXED BED TECHNOLOGY – PROVEN & PRACTICAL

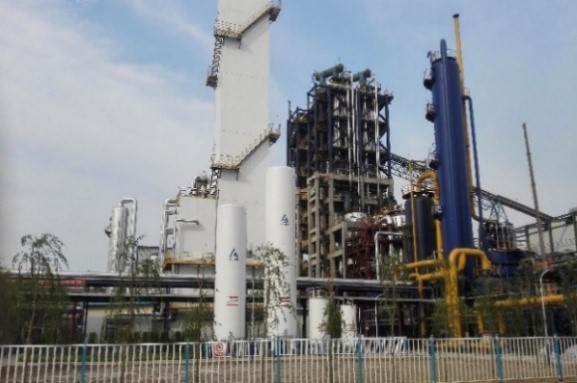
Dev Energy has developed and matured most energy Efficient and environmentally suitable solution in form of Double Stage Clean and Cold Gas technology.

KEY FEATURES:

Upstage gas -> Volatile Matter Extraction

At low temperature with CV > 1750 kcal / Nm3

Downstage gas -> Carbonised gas generation

At high temperature with CV > 1250 kcal / Nm3

The advantage of Double stage gasification is that the down stage gas being tar free can be treated in the

cyclone to remove the dust particles, then cooled through Heat exchanger and an Air cooler. The upstage gas being at cooler goes directly into ESP – Detarrer to remove tar. These Upstage and downstage gases are then mixed in indirect cooler and cooled to 45 °C. Then the final gas pass through ESP – Deoiler. The coal gas is DE-sulphurised and pressurised to the desired pressure and then transmitted to end user.

The Tar generated is clean and moisture free and can be used as fuel. The phenolic water generated is all cleaned and reused in the system itself crating a ZERO LIQUID DISCHARGE system.

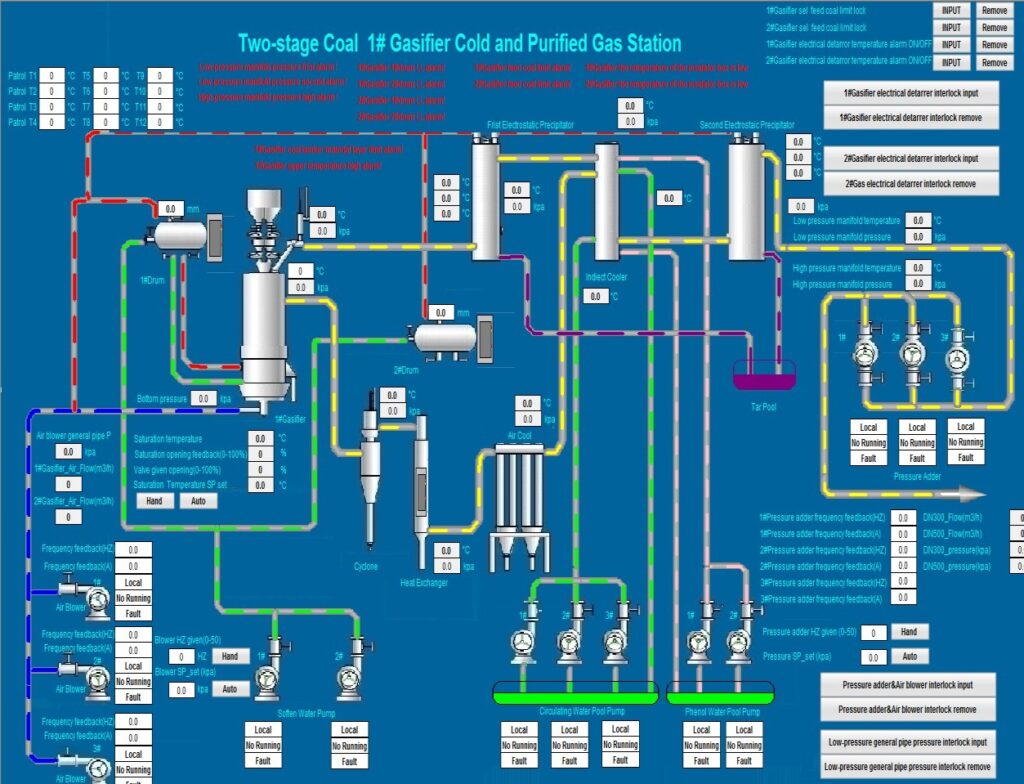
The E & A uses the latest PLC – DCS based Scada systems to Integrate, Automate the Controls making the system reliable & Safe for operations.

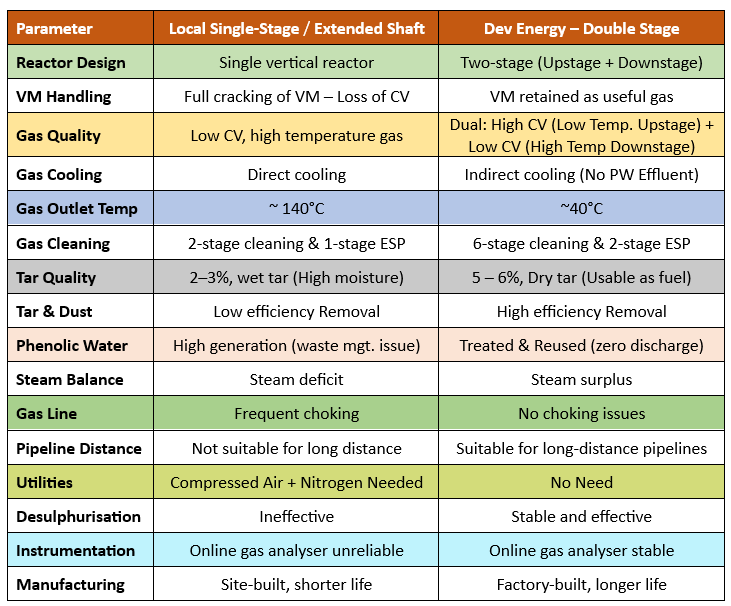
COMPARISON: DEV ENERGY VS CONVENTIONAL

CFB TECHNOLOGY – HOW IT WORKS?

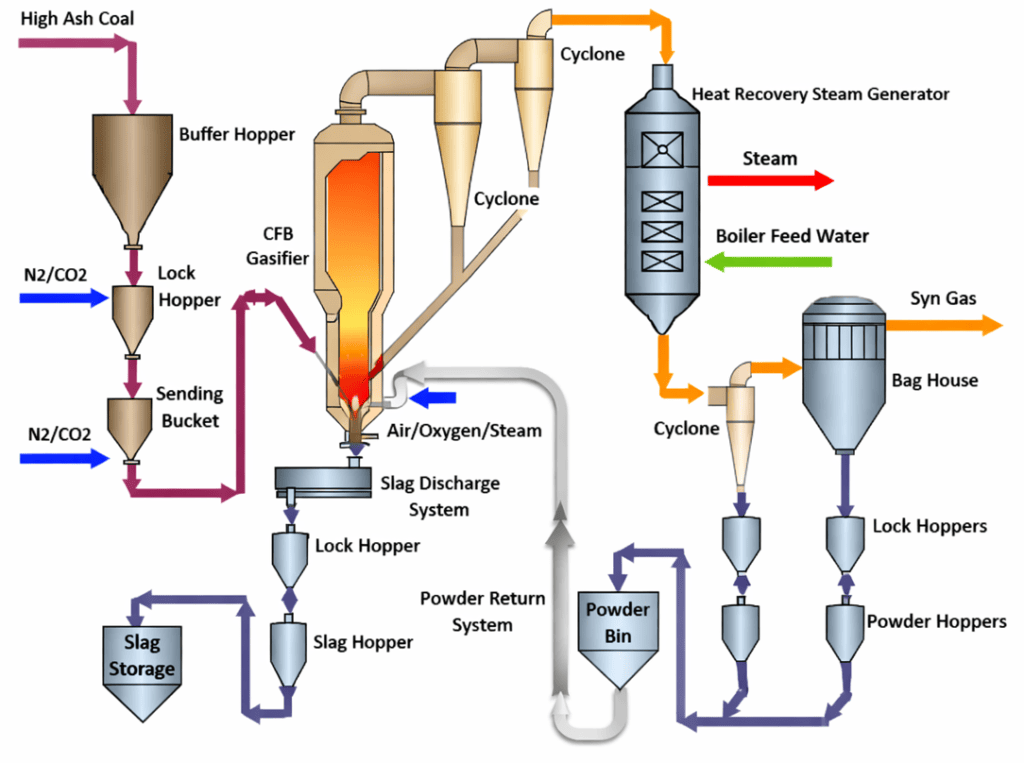
Circulating Fluidized Bed (CFB) technology is a coal gasification process where solid fuels are converted into a SYN gas at high temperature in presence of oxygen and steam. Coal is processed through grinding, sorting, and/or drying to bring the feedstock < 10 mm particulate size.

Crushed coal is pneumatically conveyed into a pressurized lock hopper, which feeds it into the CFB gasifier. The coal combines with oxygen and steam as gasification in the fluidized bed at temperature of 1000 o C to provide high carbon conversion and non-slagging of ash. Ash is removed by gravity from the gasifier and is discharged into a system for depressurization and disposal. The gasifier maintains a low level of carbon in the bottom ash discharge stream.

Fines carried over from the fluidized bed are separated from the syngas prior to heat recovery and syngas cleanup in the cyclone and bag filter. The product syngas is essentially free of tars and oils due to the temperature and residence time of the gases in the fluidized bed, simplifying downstream heat recovery and gas cleaning operations.

CFB gasification design using waste heat recovery process, which can recover the heat from syngas to produce high temperature and high-pressure steam along with oxygen preheating resulting in overall optimum thermal efficiency.

The fluidized bed design results in long residence times of the reacting particles and the fines have a two-stage recycle back process with all returning to gasifier. This helps achieve the overall carbon conversions > 98% which is among the highest in the world.

CFB TECHNOLOGY FEATURES

ECONOMICS – SAVINGS BENEFITS

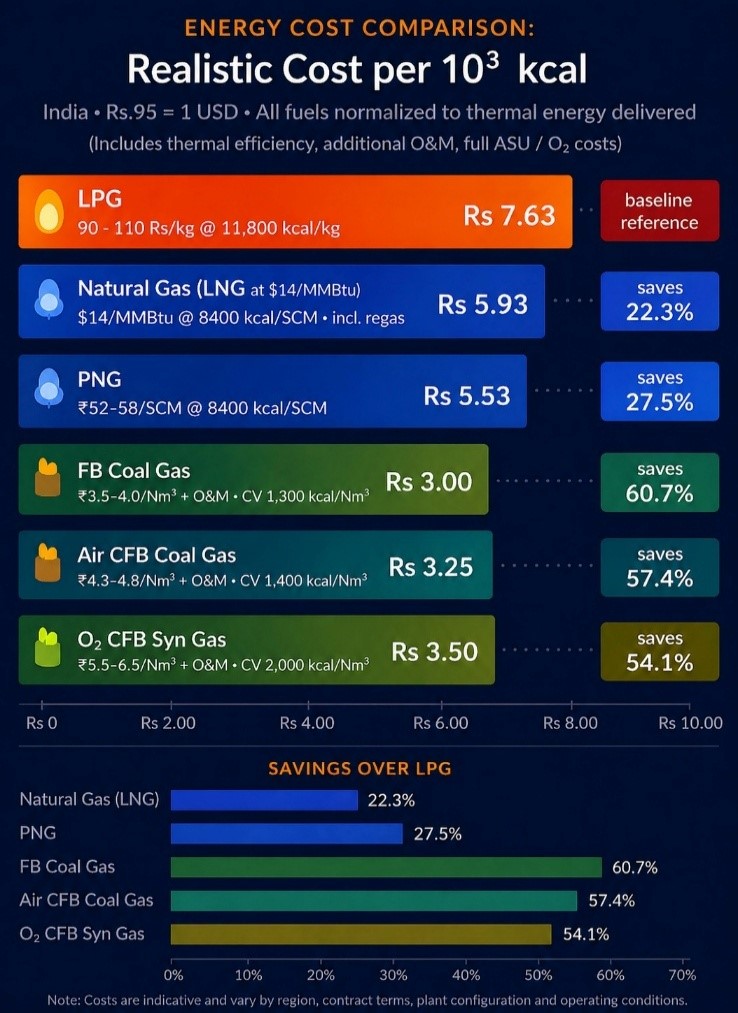
The key to adaption of COAL GASIFICATION is the acceptance of the Economic Benefits of using Indian Coal vs expensive fuels. We have developed a comparative of cost of 10,000 Kcal energy from all difference fuels as per current prices. From the table, it is clear that the real benefits are saving of more than 50% of fuel expenses.

A futuristic idea is also an integration of the coal gasification system combining Fixed Bed (FB) and Air-blown Circulating Fluidized Bed (CFB) technologies provides an efficient solution for industrial fuel generation. Lump coal is processed in the fixed bed gasifier to produce relatively clean, moderate-calorific-value syngas, while coal sizzing < 15 mm as rejects are utilized in the CFB gasifier, ensuring complete fuel utilization. Both units generate FUEL GAS primarily composed of CO, H₂, and CH₄, which is routed to a central gas network for uniform distribution across plant applications.

The use of air-blown gasification eliminates the need for an oxygen plant, significantly reducing capital and operating costs. This hybrid configuration enhances fuel flexibility, improves overall efficiency, and optimizes resource utilization. The produced FUEL GAS can effectively replace conventional fuels such as LPG, PNG, and Furnace oil in various industrial heating processes. Typical applications include steel reheating, stainless steel production, ceramics manufacturing, alumina calcination, and cement kilns.

CONCLUSION

Crude Oil derivatives and Natural gas are increasingly becoming expensive fuel options for the industry and with prices often fluctuating due to geopolitical factors and supply chain remaining uncertain, making them as the backbone of the industry is now making the complete plant dependent on unreliable energy sources.

In contrast, COAL GASIFICATION offers a stable and cost-effective alternative by converting abundant Indian coal reserves into cleaner gaseous fuel, ensuring consistent supply and economic viability.

Backed by strong expertise and operational experience, Dev Energy delivers dependable coal gasification solutions that are both affordable and efficient, positioning it as a reliable partner for sustainable energy needs. These are not claims but experience form > 250 proven commercial scale plants operating providing a ready solution in from of basic engineering, detailed engineering, and EPC solutions.

Future-Ready Low-Carbon Green Iron & Steel: CFB Coal Gasification Pathway

By UncategorizedNo Comments

Why Now?

The world is in need of processes and technologies that reduce the global carbon footprint. Every two decades steel mills need upgradation and reinvestments and in this current cycle of refurbishment, there is a chance to use low-carbon technologies that can upgrade two-thirds of the current production capacity to Green Steel before 2030. This presents a critical window of opportunity to retrofit the existing blast furnaces (BF-BOF) and Natural Gas Reforming based Direct Reduction of Iron (DRI- EAF) vertical shaft Kins with low-carbon technologies. One of the proven and available technologies is Circulating Fluidised Bed (CFB) Coal gasification with ready to use Carbon capture, Utilisation and Storage (CCUS).

What is Green Steel?

Global recognized organizations like WSA and IEA have not yet clearly defined the term green steel, instead, they define low- carbon steel in their climate change policy paper as “Steel that is manufactured using technologies and practices that enables the emission of significantly lower CO2 than conventional
production”

Currently as per global statistics, almost 71% of steel is currently being made using the BF-BOF process, with 29% produced by the EAF method. The conventional BF-BOF & Horizontal DRI Kiln routes are dependent on High-Carbon intensity raw material like coal and coke.
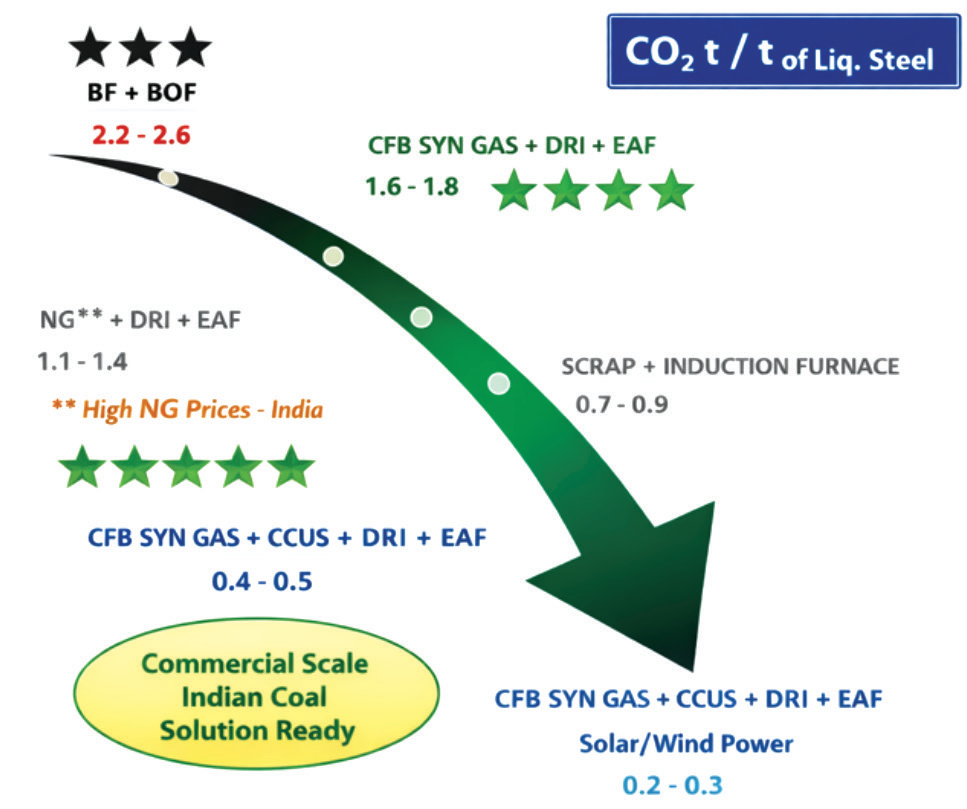
As you can see below, the Carbon Dioxide emissions from the conventional route are in the range of 2.2 – 2.6 t of CO2 /ton of steel.

Low-Carbon intensity green steel is central to achieving global decarbonization targets, as the fast-growing steel industry accounts for about 7–9% of global CO2 emissions. Now, Carbon Boarder Adjustment mechanism (CBAM) as is getting implemented globally and for steelmakers the higher CO2 intensity means higher costs directly impacting competitiveness and margins. The newer technologies can bring down the carbon dioxide emission to 0.2 – 0.3 t of CO / ton of steel.

The simplest technology that can reach the stated target is to use vertical DRI kiln where the reduction is by Synthetic Gas or SYN GAS from coal Gasification.

Basics of Low-Carbon Steel Making

As you can see from the diagram, the reduction has to happen with removal of oxygen molecules by use of carbon or hydrogen and heat has to come from either chemical of electrical energy. The key to resolving the carbon emission questions is to shift to processes that emit least carbon dioxide.

Coal Gasification generating SYN gas is the best bet for the future of steel making.

How SYN Gas is Path Forward?

Coal Gasification makes SYNGAS which is a mixture of hydrogen (H2), carbon monoxide (CO), and methane (CH4) (75 – 80% mol) with some carbon dioxide (CO2) made from coal with use of oxygen and steam firring. The basic gasification reactions are

1. C + H O → CO + H (Hydrogen)

2. C + O → CO (Carbon Monoxide)

3. C + 2H → CH (Methane)

The SYN gas generated through Coal Gasification is then cleaned and cooled through multiple stages to achieve the final state where it can be used as reduction gas for the vertical DRI kiln. Dev Energy has partnered to provide the proved technology of Circulating Fluidised Bed (CFB) gasification for the production of the SYN gas and transformation of the same to the desired specifications of stell industry.

CFB Technology – How it Works?

Circulating Fluidized Bed (CFB) technology is a coal gasification process where solid fuels are converted into a SYN gas at high temperature in presence of oxygen and steam. Coal is processed through grinding, sorting, and/or drying to bring the feedstock < 10 mm particulate size.

Crushed coal is pneumatically conveyed into a pressurized lock hopper, which feeds it into the CFB gasifier. The coal combines with oxygen and steam as gasification in the fluidized bed at temperature of 1000 C to provide high carbon conversion and
o
Coal Gasification generating SYN gas is the best bet for the future of steel making.
How SYN Gas is Path Forward?
Coal Gasification makes SYNGAS which is a mixture of hydrogen (H2), carbon monoxide (CO), and methane (CH4) (75 – 80% mol) with some carbon dioxide (CO2) made from coal with use of oxygen and steam firring. The basic gasification reactions are
1. C + H O → CO + H (Hydrogen)
non-slagging of ash. Ash is removed by gravity from the gasifier and is discharged into a system for depressurization and disposal. The gasifier maintains a low level of carbon in the bottom ash discharge stream.

Fines carried over from the fluidized bed are separated from the syngas prior to heat recovery and syngas cleanup in the cyclone and bag filter. The product syngas is essentially free of tars and oils due to the temperature and residence time of the gases in the fluidized bed, simplifying downstream heat recovery and gas cleaning operations.

Fines carried over from the fluidized bed are separated from the syngas prior to heat recovery and syngas cleanup in the cyclone and bag filter. The product syngas is essentially free of tars and oils due to the temperature and residence time of the gases in the fluidized bed, simplifying downstream heat recovery and gas cleaning operations.

CFB Technology Features & Advantages

CFB gasification design using waste heat recovery process, which can recover the heat from syngas to produce high temperature and high-pressure steam along with oxygen preheating resulting in overall optimum thermal efficiency.

CFB is more fuel-flexible with utilization of low-rank and other high-ash coals. It offers higher efficiency than competing gasification technologies. As fines carried over from the fluidized bed are separated from the syngas prior to heat recovery and syngas cleanup.

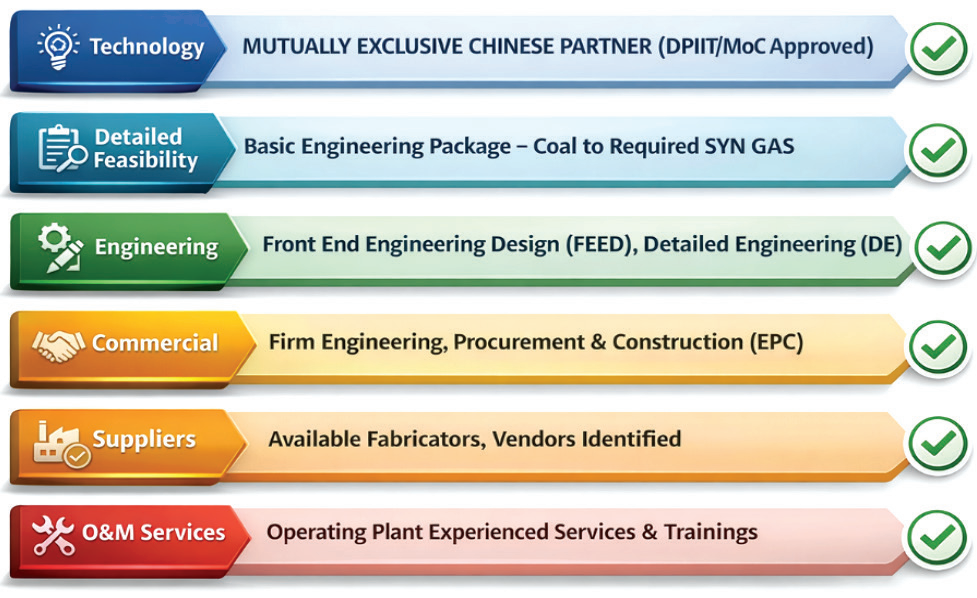
There are proven commercial scale plants operating in China and ready solution is available from basic engineering, detailed engineering, and EPC solutions

Why CFB?

Integration CFB – Vertical Kiln DRI

Dev Energy has completed the detailed study and can offer solution as required by all global vertical shaft DRI technology Licensors making it wide adaptability for overall technical and commercial optimisation to make Green Steel.

Case Study: 0.5 MTPA DRI – Vertical Shaft DRI Kiln
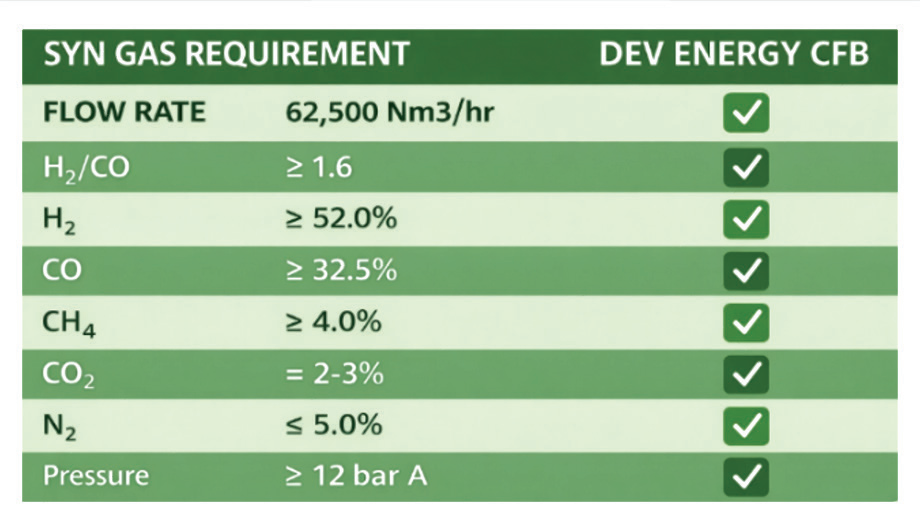
The solution is to tailor the SYN gas composition to the requirements of the DRI technology Licensors. Below are the details of requirement for the stated case study:

The SYN gas produced from the CFB gasification is transformed through the Water Shift reactor to balance the H2/CO ratio. The technology has the complete flexibility of H2/CO ratio such as 1.1, 1.6 or even future -proof 100% Blue H2.
The water shift reaction generates carbon dioxide and the amine wash technological process is used to remove the CO2 from the SYN gas. The same process also eliminates the sulphur present in form of H2S in the gas making is as per the requirement stated above.

CFB gasification adopts oxygen-enriched gasification, and the N content in syngas can be effectively controlled below 5% or lower. CFB gasification pressure is high avoiding any downstream compression requirement, and the CH content in the syngas can
4
be up to Controlled ideal for DRI steel-making feedstock.
The final simulated performance of the DRI kiln is enumerated below.

CO is threat and not COAL

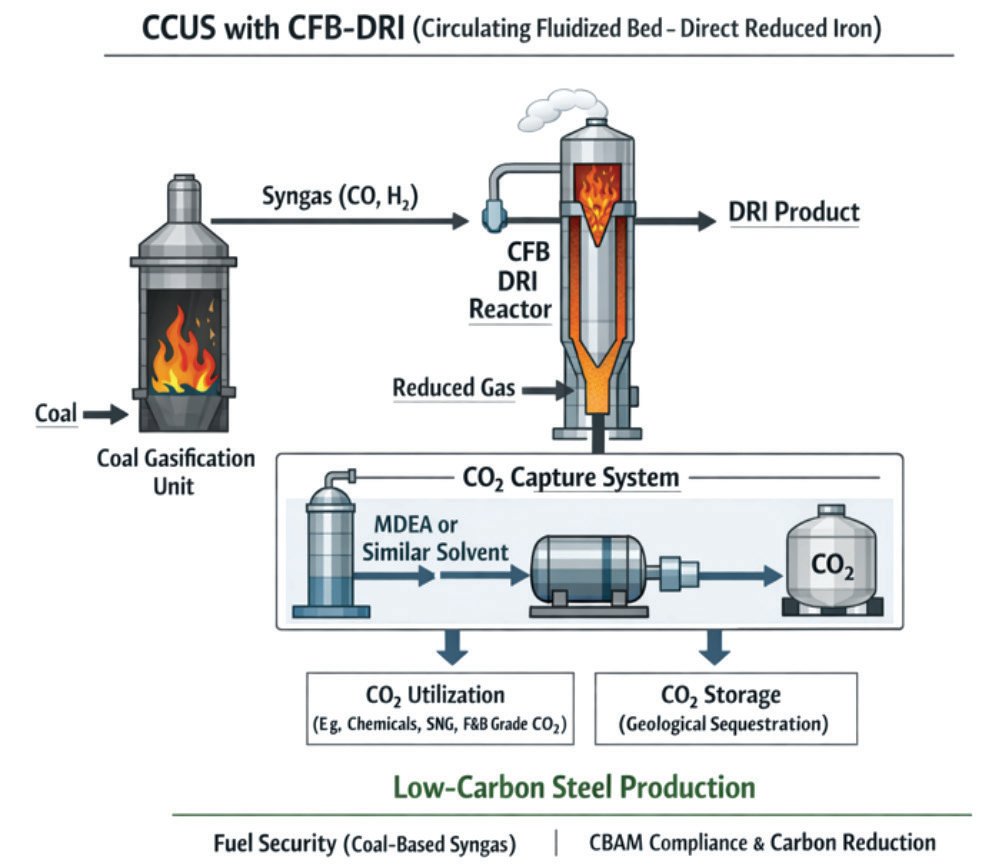
To drastically lower process CO2 emissions, CCUS with CFB- DRI (Circulating Fluidized Bed – Direct Reduced Iron) combines carbon capture systems with CFB coal gasification. In order to produce low-carbon steel, CO is isolated from the reducing gas loop using MDEA. The same is either used to make chemicals or used as F&B grade CO2 or permanently stored. This arrangement aligns DRI operations with CBAM and future carbon pricing regimes while improving the plant economics.

National Policy Support

India being 2nd largest producer of crude steel, Government of India has started offing various mechanisms of Viability Gap funding (VGF) for Coal Gasification and for Carbon Capture Utilization and Storage (CCUS). Ministry of Coal (MoC) and Ministry of Steel (MoS) have both emphasized on Low-Carbon intensity green steel making through coal gasification.

Dev Energy – Rediness:

 CFB coal gasification, optimally integrated into a vertical kiln-based downstream steel plant, will deliver green steel as shown below:

DEV ENERGY with its successful Turnkey EPC solution is ready with the complete design and implementation plan for the proven solution with exclusive partnerships already in place. We already have delivered for more than 23 years and are committed to Sustainable Low-Carbon intensity Green Steel Solutions. Dev Energy offering is through experienced & qualified team for Coal gasification and all other related infrastructure for the projects for DRI Vertical Kilns for Green Steel with committed after sales service and handholding till operational success.

Smarter Scrap Processing to enhance Steel Melting Furnace Efficiency: Case Study for West Africa

By UncategorizedNo Comments

Introduction

Steel Scrap plays a pivotal role in today’s steel making and has become the most critical raw materials in modern steel melt shops. In the world moving towards green future, there is an increasing emphasis the recycling of steel. The usage of steel scrap helps in reduction of the net carbon footprint of steel produced. The strategic use of scrap has transformed steel plants from being purely ore-based operations to circular, resource-efficient facilities. Whether it is in an Electric Arc Furnace (EAF) or in an Induction Furnace (IF) the scrap quality directly influences the productivity, metallurgy and environmental performance of the steel melt shop.

In Africa, for decades there existed a unique situation where the steel scrap was available in abundance due to the availability of war scrap and absence of steel making plants. The scrap was not used or processed and therefore available at cheap prices. The abundance did not immediately transform the industry into large scale scrap recycling-based steel melting production because of lack of any local government support or investors ready to take the opportunity. In recent years, the scenario changed completely and almost all countries have banned the export of steel scrap. All local governments have pushed investors to setup scrap recycling-based steel plants.

Initially, the abundant scrap availability and low prices resulted in steel melting practices where neither technology nor cost was considered, and only goal was to produce hot metal anyhow. Since 2022, due to the surge in steel demand and uptick in the prices of steel the industry has taken a second phase of investments and the companies are upgrading and upscaling their facilities. The maturing of markets has resulted in the newer plants shifting their focus on cost optimization, energy efficiency, and sustainability. The essential step in this exercise is to work on management of the Steel scrap with addition of the Scrap processing facilities.

Challenges of Scrap Processing in Africa

The available steel scrap in Africa is in very bad shape and form. The shapes, sizes and quality are varied and this deteriorated scrap quality has necessitated the preparation of scrap into usable scrap. This is done through scrap processing machines for achieving better efficiencies in steel melting furnaces.

The concept of Scrap processing is to undertake the following processes to achieve the desired goals.

Sort -> Process -> Clean

The goal of the processing is to get the final scrap which is

  • Sorted
  • Sized
  • Dense
  • Clean – dust free
  • Segregated

The processing of scrap can be achieved through three basic process methodologies which are shredding, shearing and baling. The suitable solution for any plant is to process the scrap in the proper parameters using machinery matching the type of scrap. The process identification depends on the type of Raw Steel Scrap, its density, its size, its cleanliness level, the size of the furnace, power density of the furnace etc. There are various types and size of machines available to process scrap from 01 to 100 t/hr.

Advantages of Scrap Processing

The processed scrap is sized, denser and cleaner for faster charging in the furnace. This processed scrap consumes less power per ton of steel produced, results in high productivity for the furnace. Power is the major cost in making steel. The scrap shape, density and size are the variables that determine the time required for melting. The input scrap that is improper results in longer time for melting and higher power consumption. Dev Energy has been actively working on reduction of power with its dynamics and interrelation to scrap processing.

Unprocessed Scrap Processed Scrap
Size Irregular Uniform
Density Low to medium High
Melting Slow & Uneven Fast & consistent
Risk Bridging none
Power Used ~ 750 kWh/ton ~ 650 kWh/ton
Yield 90 – 92% 94 – 96%
Slag Volume High Low

Dev Energy has developed expertise to provide innovative turnkey solution for efficient scrap segregation, processing and feeding in the furnace. This feeding system also has to be integrated with the pollution or Flue control system generated during melting. Our scrap solutions can be tailored to plant needs and help melting shop manage any type of input scrap; while increasing scrap value and employee safety through efficient of scrap handling. Our systems not only make scrap easier to manage, then low-cost operations reduce waste thus lowering the total cost and providing immense value to the company.

Case Study on 1000 tons / day Scrap Processing Solution in West Africa

In an era where operational efficiency defines competitiveness, a 1000 TPD induction furnace-based steel plant offers a compelling example of how smart scrap preparation can unlock measurable performance gains. Struggling with inconsistent charge material, prolonged heat cycles, and rising energy costs, the West Africa steel plant took a decisive step by inviting Dev Energy to propose and then supply the complete integrated Steel Scrap processing system.

Prior to transformation, the plant had negligible scrap processing and the unprocessed scrap handling and charging practices posed significant operational challenges that directly impacted furnace performance and overall cost efficiency. The resulting low furnace productivity driven by inconsistent scrap size and density resulted in unstable melting behaviour and prolonged heat cycles. This inefficiency was further compounded by higher power consumption as the furnace was required to compensate for dirty poor scrap and energy absorption by huge amount of slag.

In addition to above, the plant experienced notable metallic yield deterioration due to excessive oxidation and higher slag generation. Increased slag volumes also accelerated refractory wear, leading to frequent repairs and shortened lining life. Safety risks were also elevated, particularly during manual scrap handling and charging operations, while inconsistent scrap chemistry made it difficult to achieve stable steel compositions, increasing the need for corrective additions.

These technical shortcomings translated into higher maintenance requirements, unplanned downtime, and increased operating interruptions, all of which adversely affected production reliability. The heat times were extended to approximately 150 minutes per cycle, and despite the installed furnace capacity of more than 1000 tpd, the daily production remained capped at around 650 tpd.

As the first step to the designing the integrated solution, Dev Energy studied Scrap-Mix composition in terms of type of scrap, its size, density and dust levels. The plant’s input scrap was noted to be highly variable scrap mix, which created significant challenges in suggesting a consistent solution.

The scrap charge was composed of ~ 5 % HMS 1 and 20 % HMS 2, proving a limited availability of heavy, dense scrap. A substantial portion of the mix consisted of light scrap ~ 30 %. The remaining 45% comprised locally sourced unsegregated mixed scrap characterized by wide variations in size, density, quality, contamination levels and chemistry.

Solution

A detailed assessment revealed several critical pain points in this scrap mix that the plant was procuring. The average bulk density of the scrap remained low, in the range of 0.3 – 0.4 T/m. Dev Energy team mapped the scrap to the machines that can process the scrap without segregation.

BOX SHEAR 1250 TONS – FOR – HMS 1 & HMS 2

LARGE BALER 400 TON – FOR – LIGHT SCRAP

SHREDDER 1500 HP – FOR – LOCAL MIX SCRAP

Box Shear – 1250 Tons

It was identified that the input scrap HMS 1 & 2 is sourced and transported into plant in trucks which could be unloaded at one location. We proposed a Box Shear machine and calculated machine capacity of ~ 400 tpd output.

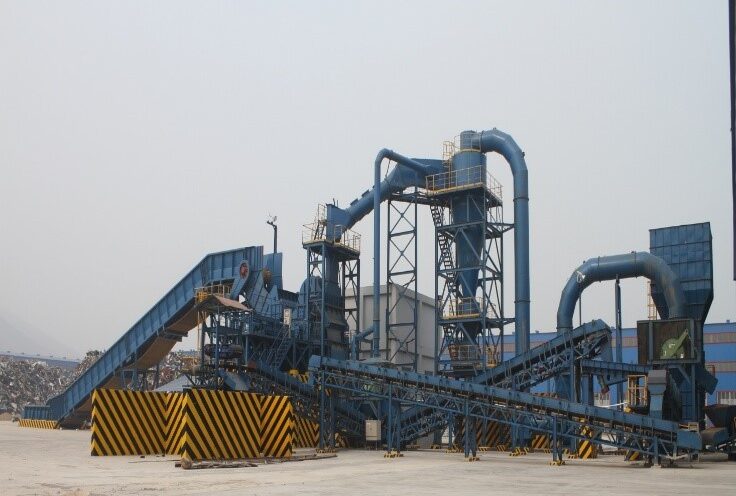
The machine is ideal for all variety of Scraps. It has the capacity for three sides of compression and additional gate side pressing & clamping. Then the desired density of scrap increased by 5 times. Finally, the Shearing blade shears the scrap into pieces of length < 350 mm with force of 1250 tons.

Shear force                         : 1250 tons

Capacity                               : 25 – 30 tph

Operation Expense         : ≤ INR 200 / t

Output Density : 1.0 – 1.2 T/m³

The machine installed is attached with a Dust Separation system integrated with magnetic separator and screening which will segregate the dust, mud, rubber, plastics and non-ferrous contaminants form the processed scrap.

Large Baler – 400 Ton

It was decided that the super light Input scrap with plate of thickness < 0.3 mm like CR punching and turning needs Baling as the same is not suitable for shearing and shredding. The estimated quantity was ~ 200 tpd and we proposed Large 3 side compression Balers.

The proposed balers will transform the light scrap into dense, consistent bales. The size of the box was taken as large with size as 3.0 m x 3.5 m and the final force of compression was 400 tons. These bales have to feed into the induction furnace so the dimensions of bales were decided as 600 mm x 600 mm x 600 mm.

Main force                          : 400 tons

Bale Weight                       : 700 – 800 kg

Bale Size                              : 600 x 600 x 600 mm      

Bale Density                      : 1.8–2.2 T/m³

Operation Expanse         : ≤ INR 125 / t

The machine installed has three sides compression, automatic PLC control, Cycle time less than 120 sec and has fully hydraulic driven operation. The main operational flexibility is for exiting the bale through Centre / Side FLIP out

Scrap Shredder- 1500 Hp

It was identified that the major input is the local mixed scrap which is sourced from multiple places and cannot be segregated. The shredder with Hammer Mill with capacity of ~ 500 tpd output was proposed.

The complete shredding line was installed with multiple stages of scrap cleaning and the machine brought a quantum leap in cleanliness and uniformity.

Output Density                 :  ~ 1.6 – 2.0 ton/m²

Output Size                        : < 90 mm

Metal Recovery                                : ≥ 99%

Operation Expense         : ~ INR 650 / t

The system was installed with the following optional add-ons

Sound Proof Enclosure

2nd Magnetic Separator

Blue Smoke Inhibitor

Video monitoring

Manual Shorting Station

Bag House De-Dusting system

Z Box Air-cleaning system

Non-Ferrous Segregation

The final output dense clean and was free of dirt & impurities.

Operational Impact

The operational impact was immediate and quantifiable. Scrap processing equipment provided the melting furnaces with uniform scrap density and cleaner scrap creating a predictable and controllable charge composition. The heat times were reduced by nearly 20 % allowing faster induction furnace turnaround and increase in the throughput by 20%. The power consumption dropped sharply delivering savings of up to 40 kWh per ton of liquid steel. The metallic recovery was observed to be much better with 1.0 – 1.5% increase in yield. The steel melt shop was cleaned and safer as fumes were less and the incidence of bridging almost disappeared. 

Financial Impact

The financial outcomes of the project were nothing short of remarkable. The project has stood out for its strong business case as the entire investment achieved payback in less than six months, reinforcing the strategic value of upstream scrap processing.

A modest ~ 1% improvement in metallic yield, at an approximate scrap cost of ~ ₹32,000 per to translated into ~ ₹ 8.0 crore per annum savings. The power consumption gains delivered even greater value with a reduction of ~ 30 kWh per ton at a power cost of ~ ₹7 per kWh resulted in nearly ₹45.0 crore per annum savings. The additional benefits arising from the reduction of the maintenance time, lower refractory consumption in furnaces and lesser accidents contributed a further ~ ₹5.0 crore annually.

Collectively, these improvements generated total annual savings in the range of ~ ₹ 50 – 60 crores against a relatively modest capital investment of approximately ₹40 crore. The result was an exceptional payback period less than 8 months which is a level of return rarely seen in steel plant modernization initiatives, firmly establishing integrated scrap processing as a high-impact, high-confidence investment.

This case underscores a broader industry lesson that the scrap is no longer just a raw material but a lever of performance which when used intelligently becomes a decisive factor in energy efficiency, yield optimization, and sustainable steelmaking. The proper selection and use of Scrap processing Machines can transform the economic viability and operational excellence of the scrap-based steel plant.

Dev Energy reaffirms its commitment to provide innovative solutions for the specific engineering-based solution designed to the specific need of the steel plants. The solutions are turnkey, reliable and cost effective making the user trust the outcome.

Walking Beam Slab Reheating Furnace with 100 % Clean Coal Gasification: Innovation in Flat Steel Rolling

By UncategorizedNo Comments

Introduction

Steel Industry in India is growing and evolving faster than ever, driven by need for lower costs, stricter emission norms, and the constant demand for better-quality. At the centre of every steel plant is the Reheating Furnace which quietly determines the energy consumption of the plant and the quality of the final product. In order to be able to meet all these demands, steel makers need to adapt innovative solution. This is where the combination of Walking Beam Reheating Furnaces and modern Coal Gasification together offer a practical, reliable and cleaner alternative to traditional fuels, while ensuring consistent and high-quality reheating.

Role of Reheating Furnaces

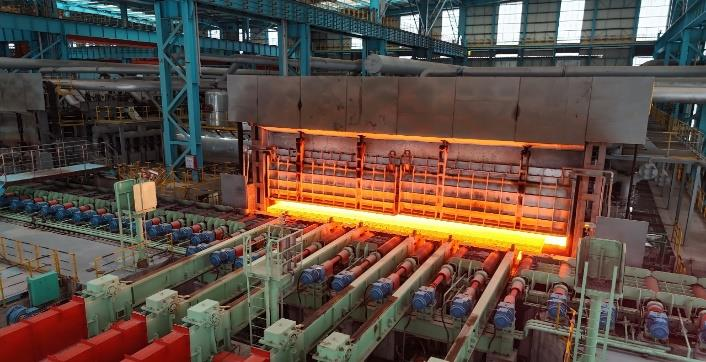
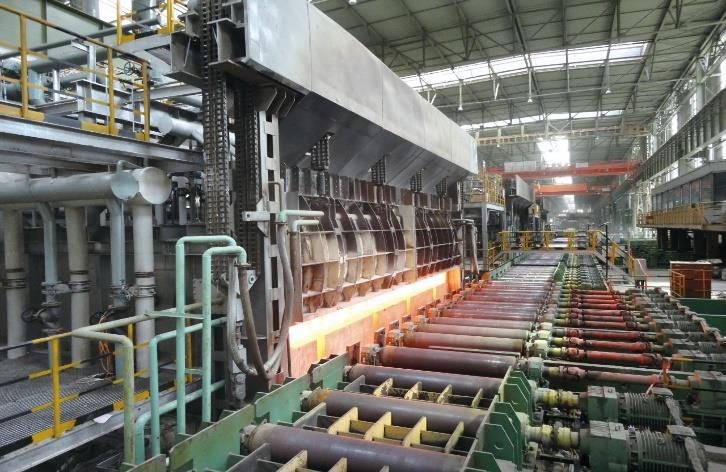
Reheating furnaces play a crucial role in the steel industry by heating the semi-finished steel products such as billets, blooms, and slabs to the required rolling or forging temperature. Reheating furnaces ensure that semi-finished raw steel materials reach the ideal temperature for deformation during rolling or forging. We must note that before these products can be rolled into final shapes, they must be reheated to precise temperatures — typically between 1,100°C and 1,250°C. This proper reheating directly affects the metallurgical properties, surface quality, and mechanical strength of the final steel rolled or forged product.

Hence, furnace design and performance have a direct impact on Quality, Productivity, Energy consumption, production cost and overall plant efficiency.

There are many types of reheating furnaces based on the configuration. The some of the important variables that define the furnace are

Variable / Parameter Types / Options
Fuel PCI / NG / LPG / Coal Gas / BF - Coke Oven Gas / Furnace Oil
RM Movement Pusher / Walking Hearth / Walking beam / Chamber / Bogie
RM In / Out Side In - out / Pusher - Ejector / Drop
Shape Floor / Top & Bottom / Neck
Burner configuration Side & front / Side Top & Bottom / Roof
Heat Recovery Recuperative / Regenerative

Why Walking Beam

In the competitive world of steel manufacturing, efficiency, product quality, and operational reliability are the cornerstones of success. The traditional reheating furnaces suffer from problems of uneven heating of the steel, high fuel consumption, and increased oxidation losses. The Walking Beam Reheating Furnace stands out as a modern, high-performance solution designed for uniform heating, improved efficiency, and superior product quality.

Its innovative design not only ensures superior heating performance but also addresses the limitations of older furnace such as pusher.

Uniform heating

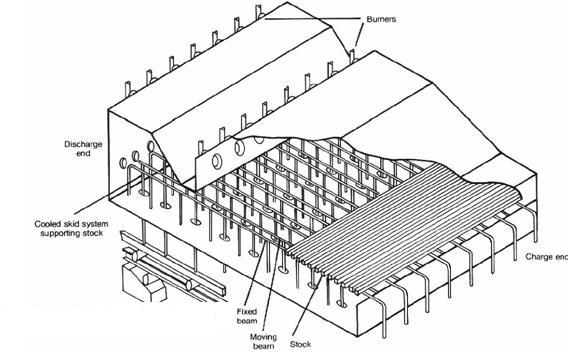
The most important and unique feature of walking beam design is the uniformity of heating across length and cross section of the material. The mechanism is designed to lift and moves the steel material step by step through the furnace. This motion ensures each billet, bloom, or slab is evenly heated on all sides, with no skid marks, maintaining consistent temperature distribution. Uniform heating minimizes internal stresses and prevents temperature-related defects, ensuring superior metallurgical quality and improved surface finish.

Flexibility

The Walking Beam Furnaces are suitable for a wide range of steel grades and product dimensions. Whether reheating long products, slabs, or blooms, the furnace can adapt to different production needs. The flexible control of heating zones and temperature profiles allows operators to fine-tune the process according to specific steel grades—making it equally effective for all steel grades hearting including speciality steel, Mild Steel and Stainless-Steel material reheating in the same furnace.

High efficiency

Walking Beam Reheating Furnaces are designed for optimal thermal performance. They utilize advanced combustion systems, waste heat recovery units, and efficient insulation to minimize energy loss. Th oxidation losses in the operation of the furnace are minimum. The combination of regenerative or recuperative burners significantly reduces fuel consumption, leading to lower operating costs and improved energy efficiency. This high thermal efficiency contributes directly to sustainable and cost-effective steel production.

Low maintenance

The mechanical components of a walking beam system operate smoothly with minimal friction. Because the steel is lifted rather than pushed, wear and tear on the furnace hearth are greatly reduced. This leads to lower maintenance costs, less downtime, and extended equipment life. The possibility of billet / Slab rotation or movement is minimum. The design also allows easy access for inspection and servicing, enhancing reliability and productivity.

Key Considerations for SS Steel production

For stainless steel, precise temperature control and a clean heating environment are essential. The walking beam design prevents surface scratching and oxidation, ensuring high-quality SS billets and bars with excellent surface finish and mechanical properties. The accurate flame length and consistent temperature control across all furnace zones is critical. Managing the furnace atmosphere is especially important in stainless steel reheating. Controlled oxygen levels prevent scaling and surface oxidation, maintaining the cleanliness and quality of the steel surface.

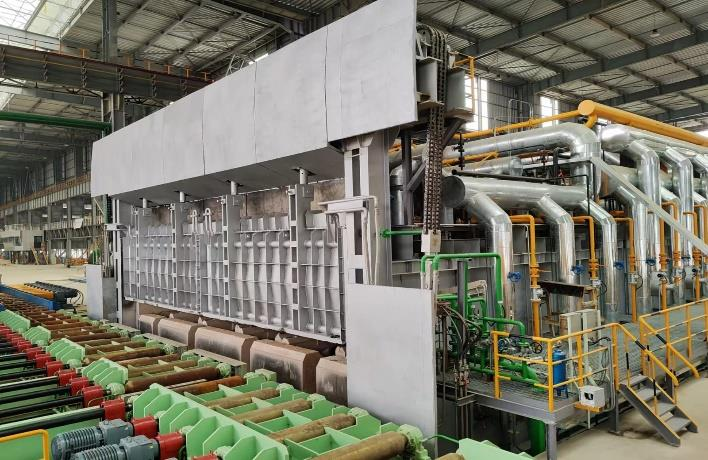
Integration of coal gasifier with walking beam CADRE – RHF POWERHOUSE Reheating Furnace

In today’s steel industry, the focus is steadily shifting toward sustainable and cost-effective energy solutions. One of the most innovative advancements in this the usage of Clean and Cold Coal Gas which can be generated from the local Indian coal. The important step in the development of same in India is the integration of a Coal Gasification with the Walking Beam Reheating Furnace. This combination not only improves the overall thermal efficiency of steel reheating operations but also
significantly reduces fuel costs and environmental emissions.

A coal gasifier converts solid coal into coal gas, a mixture of carbon monoxide (CO), hydrogen (H₂), and methane (CH₄), which is then cleaned of the impurities like tar, dust and sulphur. The resulting gas contains fewer particulates, lower sulphur content, and reduced greenhouse gases. The clean gas burns more efficiently and cleanly compared to other fuels. When used as a fuel for reheating furnaces, this gas ensures better combustion control, uniform heat distribution, and reduced fuel wastage. The result is lower energy consumption per ton of steel produced and improved operational consistency across the furnace zones.

Coal gas has a lower carbon intensity than solid coal combustion, which translates to reduced CO₂ and particulate emissions. Additionally, the controlled combustion process produces less smoke, dust, and unburned carbon, helping the steel plant meet stricter environmental regulations. This integrated system also minimizes the formation of scale and oxidation on steel surfaces, improving product quality while maintaining cleaner furnace conditions.

Founded in 2000, Shanghai Cadre Industrial Furnace Co., Ltd. (CADRE) is a leading enterprise specializing in EPC for metallurgical industry furnaces and kilns. With five R&D and engineering centres located in Shanghai, Beijing, Shenyang, and Anshan, and three manufacturing bases in Anshan, CADRE employs nearly 300 professional R&D engineers and 300 skilled technical workers. The company’s integrated capabilities span design, equipment manufacturing, project management, and on-site construction.

Over the past 25 years, CADRE has successfully executed more than 1,000 projects across China and overseas, maintaining a 100% success rate. The company holds multiple national patents, has received provincial and ministerial-level science and technology awards, and is recognized as a National High-Tech Enterprise. With the largest industrial furnace manufacturing facility in China, CADRE can produce up to four to five complete walking beam furnaces per month, ensuring strict quality and delivery standards.

CADRE pioneered dual-regenerative combustion technology for low-calorific-value gas and single-regenerative technology for high-calorific-value gas, achieving industry-leading energy efficiency and ultra-low NOx emissions. CADRE operates advanced industrial experimental platforms and continuously develops next-generation technologies such as low-NOx burners, full-oxygen combustion, and modular furnace construction methods. The company holds essential qualifications for metallurgical design and construction, along with ISO 9001, ISO 14001, and ISO 45001 certifications, ensuring compliance with global standards of quality, safety, and environmental management.

DEV ENERGY – COAL GASIFICATION

DEV ENERGY is the hub for innovation and since 2001 we have been implementing solutions for efficiency and productivity enhancement in the steel, glass, aluminium and ceramic industries with over 300 systems operating successfully saving crores for our users. We pride ourselves on providing complete tailor-made turnkey solutions.

We have 24 years of experience in the domain of Coal Gasification and have undertaken most of India’s first projects for Coal Gas generation. The system, processes and the equipment are designed and engineered by experienced and professional engineer from India and China.

Technology Advantages

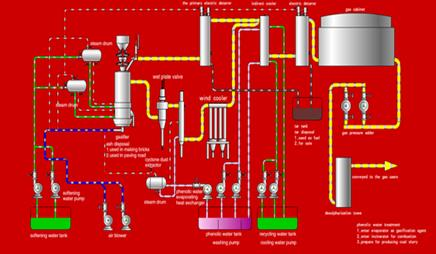
The heart of the technology is the double stage gasification process where the Volatiles in the coal are separated in the Upstage reactor and the fixed carbon in coal is converted into the carbonised gas. The purification process uses seven stages of cleaning and cooling of gas with three stages of closed cycle indirect cooling including air cooler and indirect water cooler are used to cool the gas. The two stages of electrostatics precipitation are used to clean the gas of tar. Dust is removed by cyclone. The seventh stage of sulphur removal is done using desulphurisation tower.

The need for water scrubbing is eliminated and all cooling is done without direct contact with water. This eliminates generation fresh water in to phenolic water. A specially designed heat exchanger is used to vaporise the condensate moisture and phenols which are injected back to the gasifier. This technology of reusing the phenolic water helps save energy and uses the phenolic water back in to the system. The technology complies with the norms of pollution control board. The system is designed for 100% water and steam reuse and no water of any type is discharged outside the system limit making it a zero-discharge system.

The tar produced by the process of dry electrostatic precipitation is at low temperature and free of moisture. This tar is a high-quality tar with CV > 8500 Kcal / Kg.

Process Flow Diagram

The technology because of its non-contact nature making it much safer to operate. It is also very user friendly for and provides consistent performance. The automation helps to continuously monitor the quality and quantity of gas which feed the Algorithmic based programming to increases the overall efficiency of the system.
The safety of the system is ensured with a combination of fast cut off valves with high-speed vents for gas release and a highly responsive signal interlocking system programmed into the PLC system.

The clean gas improves the life of the furnaces and the burning systems.

Walking Beam Reheating Furnaces integrated with Clean Coal Gasification is a solution that bring together everything steel producers need today — a lower fuel bill, better control on heating, reduced emissions, and a stable, predictable operation. The system makes it easier for steel plants to deliver high-quality steel at lower costs while meeting sustainability goals. As India’s steel industry prepares for a new phase of growth, this combination offers a clear, future-ready solution. With a strong foundation in engineering and proven gasification expertise, DEV ENERGY is proud to support this transition and help steelmakers move confidently toward cleaner and more efficient production.